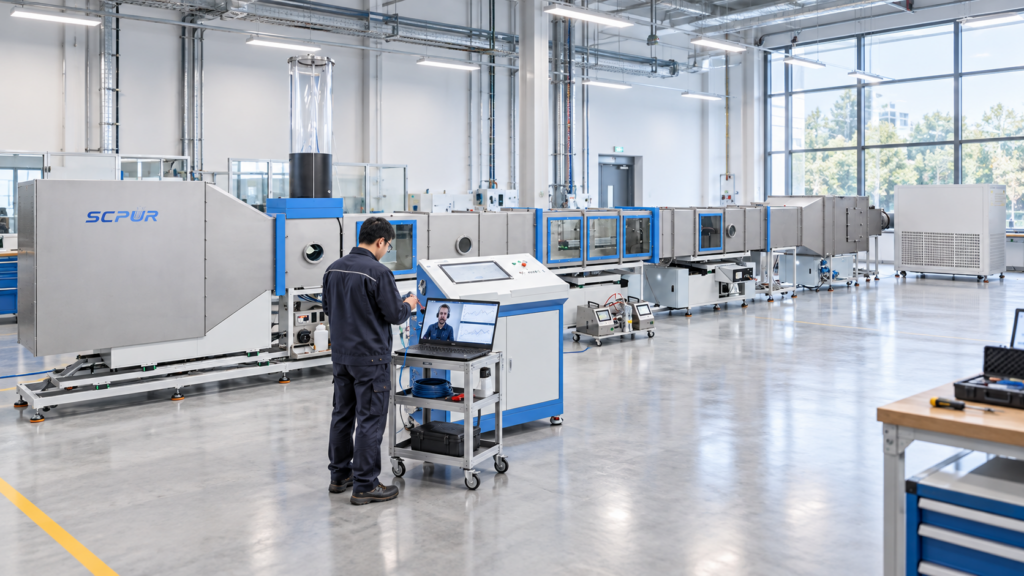


An ISO 16890 test is not a one-point efficiency measurement followed by a rating. The complete workflow combines airflow and resistance, initial fractional efficiency, performance after the specified conditioning procedure, and, when required, dust loading. Each stage answers a different question and must be reported correctly.
The core test workflow
The core test workflow
- Set the test airflow and measure pressure drop. Airflow must remain stable, and the test duct must be checked for leakage and unacceptable flow distortion.
- Measure initial fractional efficiency. Upstream and downstream particle concentrations are used to build an efficiency curve across particle-size intervals rather than one value at 0.3 µm.
- Condition the filter as specified in ISO 16890-4 and repeat the fractional-efficiency measurement. The purpose is to evaluate performance after removable electrostatic effects have been reduced, not to reproduce field aging.
- Apply the standard reference particle distributions and calculation rules to determine the ISO ePM1, ePM2.5, ePM10 or ISO Coarse group and rating.
- When dust-loading performance is required, conduct the ISO 16890-3 test and record gravimetric efficiency and resistance against captured test-dust mass. Report this separately from ePM classification.
What must the test rig control?
What must the test rig control?
Accuracy depends on more than the particle counter. The system must control airflow, aerosol concentration and mixing uniformity, upstream and downstream sampling, sampling-line losses, pressure measurement and background concentration. For higher-efficiency samples, the downstream concentration must remain above the instrument detection limit. Dilution errors and switching delays can otherwise create convincing but incorrect results.
Four common reporting errors
Four common reporting errors
- Treating a fixed-particle-size efficiency as ePM1 or ePM2.5.
- Describing conditioned efficiency as the efficiency after several months of service.
- Using a dust-loaded efficiency value in the final ePM classification.
- Checking instrument certificates while ignoring validation of the duct, sampling and calculation chain.
How should the laboratory be configured?
How should the laboratory be configured?
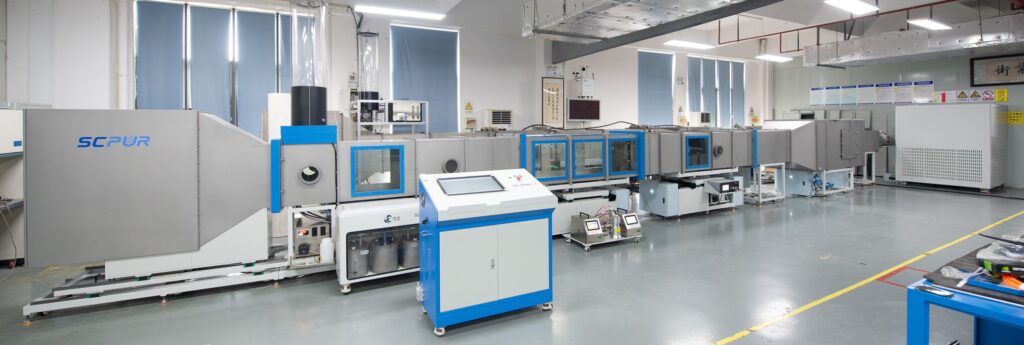
A laboratory issuing complete classifications normally needs fractional-efficiency and resistance testing together with the specified conditioning capability. Dust loading is added when ISO 16890-3 results are required. A production-control method may be faster and simpler, but its output should not be presented as a complete ISO 16890 classification. The SCPUR SC-16890 configuration should therefore be selected from the sample dimensions, airflow range, conditioning and dust-loading scope, reporting needs and the customer’s existing calibration system.