

W 1822 is the European standard used to classify high-efficiency air filters for ventilation, air-conditioning and technical processes such as cleanrooms and pharmaceutical manufacturing.
The standard covers three filter groups:
- Group E: Filtry EPA
- Grupa H: Filtry HEPA
- Group U: ULPA filters
This article refers to EN 1822-1:2019, which defines classification, testowanie i znakowanie wydajności. The detailed procedures for aerosol generation, pomiar cząstek, filter-media testing, filter-element leakage and overall efficiency are referenced through ISO 29463 Strony 2 Do 5.
Why Does EN 1822 Use MPPS?
W 1822 evaluates filters at the most penetrating particle size, lub MPPS.
MPPS is the particle size at which a particular filter medium has its lowest filtration efficiency under the specified test conditions. It is determined from a fractional-efficiency curve rather than assumed to be one fixed particle diameter.
For many glass-fibre filter media, MPPS is often found within a submicrometre range. Jednakże, it should not automatically be stated as 0.3 µm. The actual result depends on the filter medium, face velocity and particle-capture mechanisms.
Testing only at a fixed 0.3 µm channel may be useful for a validated production quality-control method, but it is not automatically equivalent to formal EN 1822 klasyfikacja w MPPS.
W 1822 Filter Classes
W 1822 classifies filters according to their efficiency or penetration at MPPS.
| Grupa filtrów | Klasa | Minimalna sprawność całkowa przy MPPS | Minimum local efficiency at MPPS |
| EPA | E10 | 85% | Nieużywany do klasyfikacji |
| EPA | E11 | 95% | Nieużywany do klasyfikacji |
| EPA | E12 | 99.5% | Nieużywany do klasyfikacji |
| HEPA | H13 | 99.95% | 99.75% |
| HEPA | H14 | 99.995% | 99.975% |
| ULPA | U15 | 99.9995% | 99.9975% |
| ULPA | U16 | 99.99995% | 99.99975% |
| ULPA | U17 | 99.999995% | 99.9999% |
Group E filters are classified using integral efficiency and are not leak-tested for classification purposes.
Groups H and U require both integral performance and compliance with the applicable local penetration limit. The standard does not require physically “zero leakage.” It requires that local penetration does not exceed the limit specified for the relevant class and method.
Three Different Test Tasks
A complete EN 1822 evaluation involves related but distinct test tasks.
1. Filter-Media Testing
A flat-sheet media sample is tested across a particle-size range at the specified media velocity. The fractional-efficiency curve is used to identify MPPS and evaluate the performance of the filter medium.
Media testing is useful during material selection and product development, but it does not classify the finished filter.
Pleating, adhesive application, framing, sealing and handling can all affect the performance of the completed product.
2. Integral Filter Efficiency
The finished filter is tested at its nominal airflow. Upstream and downstream particle concentrations are measured to determine the average efficiency or penetration of the complete filter element at MPPS.
Pressure drop is also recorded at the nominal airflow.
Integral efficiency represents the average performance of the whole filter. A filter can meet its integral efficiency requirement and still contain a localized defect.
3. Local Leak Testing
Local testing checks the downstream filter surface and relevant sealing areas for points where penetration exceeds the permitted limit.
Possible defects include:
- Damage or pinholes in the filter medium
- Adhesive discontinuities
- Leakage between the media pack and frame
- Manufacturing or handling damage
In a particle-counting scan test, a sampling probe moves across the downstream face of the filter. Reliable results depend on complete scanning coverage, controlled probe speed, odległość sondy, sampling flow and stable upstream aerosol concentration.
A scan test is therefore more than moving a particle counter across the filter surface.
What Controls the Accuracy of the Test?
Reliable EN 1822 testing requires the complete measurement system to operate under controlled conditions.
Important factors include:
- Stable test airflow
- Correct filter installation and sealing
- Suitable aerosol generation at the required MPPS
- Uniform upstream aerosol concentration
- Reprezentatywne pobieranie próbek z góry i z dołu
- Particle-counter sensitivity and concentration range
- Appropriate dilution when required
- Low background particle concentration
- Controlled scanning speed and probe geometry
- Complete scan coverage
- Correct calculation and reporting logic
The required detector sensitivity becomes increasingly demanding from H13 through U17. Equipment suitable for routine H13 production testing is not automatically capable of accurately evaluating U16 or U17 filters.
Factory Testing and Installed-System Testing Are Different
W 1822 classification is performed on the filter element under defined test conditions.
An installed-filter integrity test checks the filter after installation in a cleanroom, air-handling unit or other system. It can detect bypass leakage through the gasket, uszczelnienie żelowe, mounting frame or housing.
Installed integrity testing does not replace the manufacturer’s factory classification test. Likewise, a factory filter scanner and a portable photometer used for field integrity testing are not the same type of equipment.
What Should Be Defined Before Selecting Equipment?
Before selecting an EN 1822 systemu testowego, potwierdzać:
- The required filter class
- Maksymalne wymiary filtra
- Nominal airflow and pressure-drop range
- Expected MPPS range
- Testuj aerozol
- Required particle-measurement sensitivity
- Whether the task is media testing, integralna wydajność, leak scanning or a combination
- Required production throughput and automation
- Report format and customer acceptance criteria
Stating only that equipment “supports EN 1822” is not enough. The actual test scope, filter class and measurement capability must be defined.
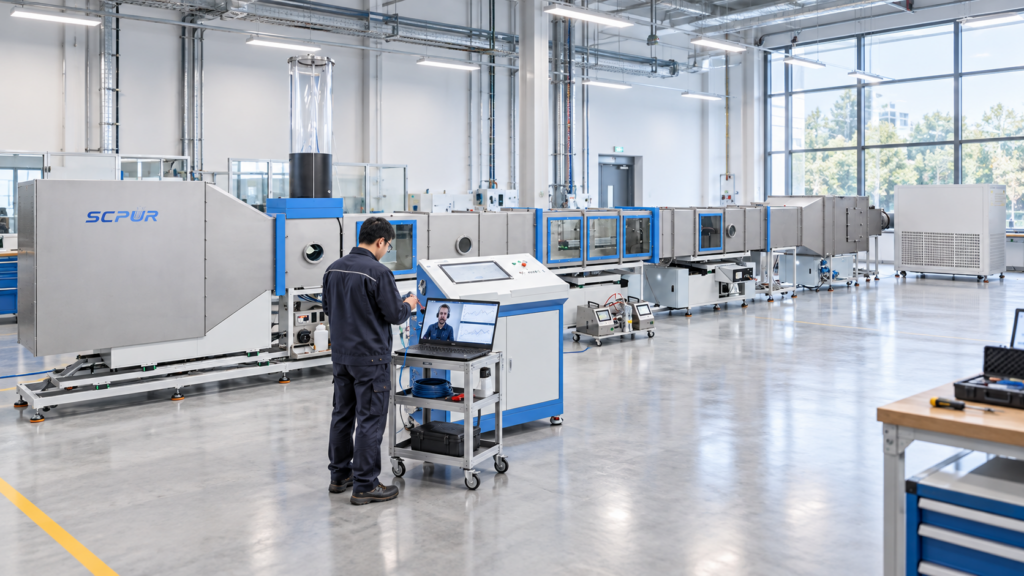
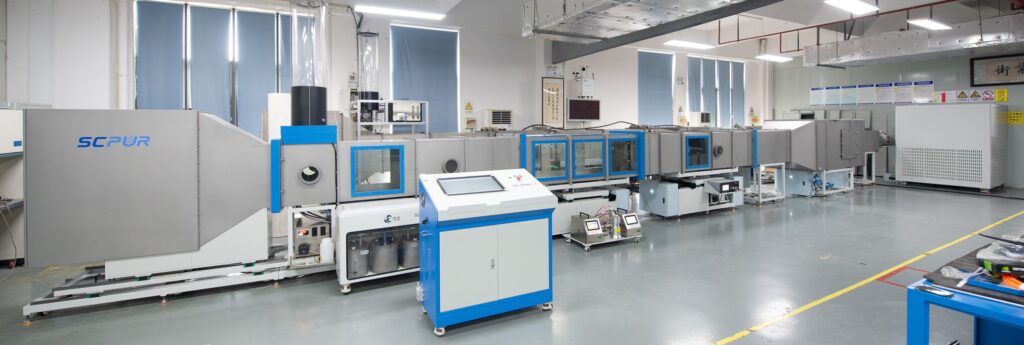
SCPUR provides separate solutions for flat-sheet filter-media evaluation and factory testing of finished EPA, Filtry HEPA i ULPA. The SC-L8023/U series supports controlled factory scanning and production testing according to the required filter size, przepływ powietrza, particle-measurement range and test procedure.